
- 1. What Microcellular Polyurethane Means in a Cast Bump Stop
- 2. Why Density Moves the Curve More Than Hardness Does
- 3. The Four Structural Variables You Can Specify
- 4. Three Curves From One Compound: A Reading Exercise
- 5. Checking Cell Structure Without a Laboratory
- 6. When Cell Structure Is the Root Cause: Five Signatures
- 7. Specifying Microcellular Polyurethane on a Drawing
- 8. Frequently Asked Questions
- 8.1. Can I specify microcellular polyurethane by density alone?
- 8.2. Why does a bumper read the right hardness and still sag after a season?
- 8.3. Is a lower-density part always softer near the top of the stroke?
- 8.4. Does cell structure change the temperature behaviour of microcellular polyurethane?
- 8.5. How do I check density on a delivered carton without cutting a part?
- 8.6. What is the difference between porosity and a cellular structure?
Microcellular Polyurethane: Cell Structure Sets Stiffness
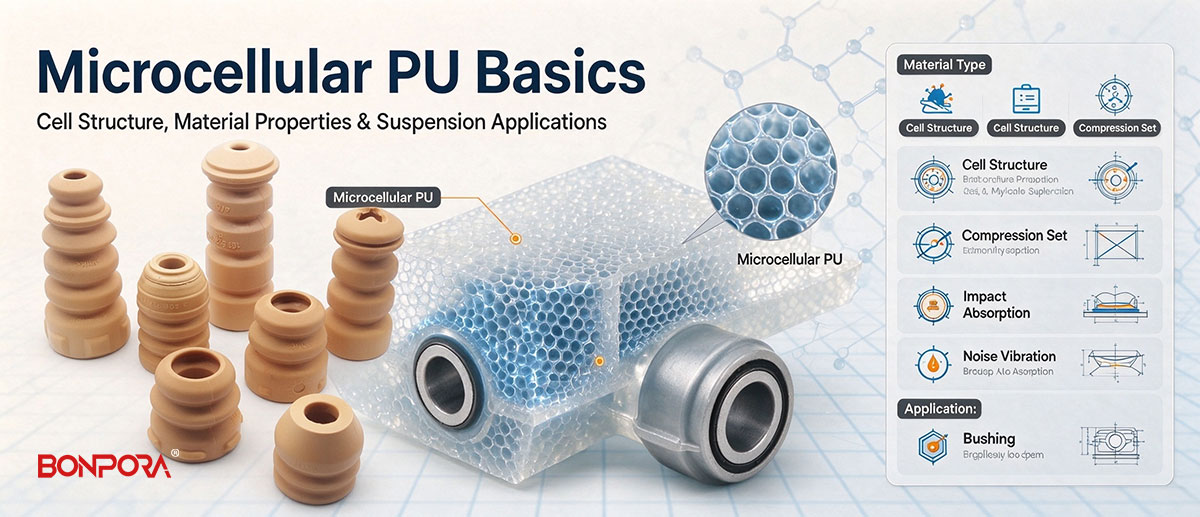
Microcellular polyurethane sets bump stop stiffness through four structural variables rather than one: density, cell size, the denser skin at the mould face, and the share of cells that stay closed. A 20 per cent density change on the same profile moves the curve by roughly 40 per cent. This guide shows how to read that relationship and write it into a drawing.
What Microcellular Polyurethane Means in a Cast Bump Stop
The reaction that builds the polymer also releases gas. In a closed mould the gas expands the reacting mass until it fills the cavity, so the part comes out with a cellular core and a dense skin where the material met the tool. The skin forms because the wall runs cooler than the core, and the surface sets before the gas can expand it.
Bonpora describes its jounce bumper as high-elasticity polyurethane in an MDI or NDI system, cast, post-cured and inspected on four items: static stiffness curve, compression set, hardness and appearance, under an IATF 16949 quality system. Microcellular describes the cell scale, not the chemistry. The cells are small and mostly closed, so the part still behaves as a structural spring rather than a cushion.
Three consequences follow, and each one changes how a specification should be written.
The part is a composite of skin and core. Skins carry a disproportionate share of the load in small parts, because their volume fraction is high.
Density is a design variable. In a solid rubber stop the density is fixed by the compound. In a cast cellular part it is set by shot weight, mould temperature, gas generation and packing, so it can be tuned to a curve and it can drift away from one.
The same mould does not guarantee the same part. Profile, free height and compound can all be held while density moves, and the curve follows the density.
Density is invisible in a photograph, cheap to measure, and rarely written on a purchase drawing. That is the gap this article is about.
Why Density Moves the Curve More Than Hardness Does
Hardness is a surface measurement, taken on the finished part and usually on a flat area, because an unsupported reading on a rib comes out misleadingly low. Density is a through-section property, and it counts the cells that carry nothing. Two parts can read the same 70 Shore A and behave differently.
The link between them is relative density: part density divided by the density of the solid polymer. Trade figures for solid cast polyurethane sit near 1.10 g/cm³, and trade figures for cellular bumper compounds commonly sit between 0.45 and 0.65 g/cm³, so a typical part runs at a relative density of roughly 0.40 to 0.60. Confirm those numbers for your own compound rather than carrying them across programmes.
In the standard model of cellular solids, modulus falls with the square of relative density when cell faces are open. When cells stay closed, the faces stretch and the trapped gas resists compression, so the exponent drops toward 1. Cast microcellular polyurethane sits between those cases, which is why a measured curve beats a calculated one.
The arithmetic still explains the sensitivity. Take a part at 0.60 g/cm³ and reduce it to 0.48 g/cm³ on the same profile:
Relative density falls from about 0.55 to about 0.44, against a solid at 1.10 g/cm³.
The ratio is 0.80, and the square of that ratio is 0.64.
At the same deflection the part would be expected to lose roughly a third of its stiffness.
Run it the other way and the same sensitivity becomes a risk: a 20 per cent overshoot gives 1.20 squared, or about 44 per cent more force at a given deflection, felt as a harder arrival and less useful travel.
The Four Structural Variables You Can Specify
Density has the largest effect, but it is not the only item that belongs on a drawing. The wording column is written the way it should appear in a purchase specification.
| Structural variable | How it is measured | Effect on the stiffness curve | Wording that works on a drawing |
|---|---|---|---|
| Density | Part mass divided by part volume, on five parts | Moves the whole curve up or down; the dominant lever | Nominal density with a tolerance, plus part mass with a tolerance |
| Cell size | Section cut, against a scale or a reference photo | Coarse cells collapse earlier and densify more abruptly | Cell size band, or a section photograph as the standard |
| Skin | Section cut, measured at three points | Raises force at small deflection and protects the surface | Skin continuous on the load face; section photo on the first-article report |
| Closed-cell content | Section cut and immersion, or a process record | Limits how fast stiffness falls as density drops | Closed-cell structure, no open network on the load path |
| Cell uniformity | Visual comparison with the approved section | Uneven cells give a curve that varies between samples | No band of coarse cells; no void above the agreed size |
| Free height | Height gauge on the finished part | Sets where the stop engages in the stroke | Free height with tolerance, measured on the part, not the mould |
The order is deliberate. Density and free height can be checked with a balance, a calliper and a height gauge, so they can be checked on every batch. Cell size, skin and closed-cell content need a section cut, so they belong on the first-article report and on periodic re-verification.
Request a specification sheet or a sample section and the four variables can be checked against the curve your application needs, rather than against a hardness number carried over from another programme.
Three Curves From One Compound: A Reading Exercise
The table shows the same compound and the same nominal profile at three densities. The numbers are illustrative, built to show the shape of the relationship rather than to describe any production part.
| Density, g/cm³ | Force at 25 per cent deflection, N | At 50 per cent, N | At 75 per cent, N | At 85 per cent, N | How it reads on the vehicle |
|---|---|---|---|---|---|
| 0.46 | 210 | 620 | 1,680 | 3,400 | Soft arrival; long useful travel; more stroke before load builds |
| 0.55 | 285 | 840 | 2,280 | 4,600 | The middle case: progressive without a sharp knee |
| 0.62 | 340 | 1,010 | 2,740 | 5,540 | Firm early; the knee arrives sooner; less travel before densification |
Three readings matter. First, the gaps widen as deflection rises: about 130 N between softest and firmest at 25 per cent, about 1,060 N at 75 per cent, so a comparison made at one point is easy to pass and easy to miss.
Second, the shape is not a straight line, and should not be. A cellular part bends and buckles its cell walls at low strain, then stiffens sharply as the cells collapse and the material densifies. That knee is the progressive behaviour the part is chosen for, and it is what a hardness reading cannot describe.
Third, density alone does not decide the curve. A 0.46 g/cm³ part with a thick skin can produce more force at 25 per cent than a 0.55 g/cm³ part with a thin skin, because the first millimetres of travel load the skin rather than the core. That is why the same density from two suppliers is not the same part, and why the section photograph belongs beside the curve.
The curve is also one of the four items Bonpora inspects on every batch sample, which means the acceptance test already in place captures cell structure without naming it. A buyer who wants structure controlled does not need a new test method; the buyer needs the existing curve test tied to a density and a section reference.
Checking Cell Structure Without a Laboratory
Most buyers have no sectioning rig, and none is needed to catch the common problems. The sequence below uses a 0.01 g balance, a calliper, a height gauge, a sharp blade and the approved first-article section. It takes about three and a half hours for a first article.
Weigh five parts from different positions in the shipment on a balance readable to 0.01 g, recording each mass separately. A spread inside one carton is a signal.
Measure the envelope with a calliper at three stations on each part and calculate volume. On a simple shape this separates 0.46 from 0.55 g/cm³.
Divide mass by volume and compare with nominal density. On small parts expect a slightly high figure, because the skin is a larger share of volume.
Cut one part through the load axis in a single firm pass of a sharp blade. A saw smears the cells; a slow blade tears the walls.
Read the cell distribution against the approved photograph. A band of coarse cells in the load path softens the knee, then stiffens it abruptly.
Measure the skin at three points on the cut face: load face, waist and base. Depth varies with mould temperature and shot weight; a face with no skin at all does not.
Check rib roots and the bore for voids and knit lines, the features that turn a cosmetic defect into a fatigue origin.
Compare with the first-article photograph at the same magnification. This is the step most inspections skip, and the one that catches a compound change.
Run the curve at 25, 50 and 75 per cent deflection against the first-article reference, not a catalogue value.
Record batch code, mass, density and the section photograph in the receiving record, so a claim six months later is answered with data.
The order runs from cheap to expensive. Where a supplier cannot support step 9, the first-article report should at least carry density, mass and the section photograph, because anyone with a balance can re-check those three.
For the production side of the same question, the jounce bumper manufacturing guide sets out the casting route, the cure and post-cure stages, and the defects worth auditing.
When Cell Structure Is the Root Cause: Five Signatures
A curve that misses its reference has several possible parents, and cell structure is only one. The table separates the signatures that point to structure from those that point to cure, tooling or the drawing. Getting this wrong sends a buyer back to a supplier with the wrong question.
| Signature on the report or the part | What it points to | First check | Often confused with |
|---|---|---|---|
| Curve rises early across the range, part mass above nominal | Density overshoot or overfill | Part mass against drawing on five parts | A profile trimmed long |
| Soft knee, then a sharp step at high deflection | Coarse cells in the load path | Section cut and cell size band | A softer compound |
| Curve correct when new, force drops after 70 h at elevated temperature | Compression set, usually incomplete cure | Cure and post-cure records for the batch | A density problem |
| Height below nominal, curve shifted left | Free height or trim setting | Height gauge on the part | Mould wear alone |
| Voids or a coarse band at a rib root | Moisture in the components or incomplete degassing | Drying and vacuum records | Release agent build-up |
| Curve varies between samples in one batch | Mould temperature distribution, uneven cell gradient | Mould heat map and shot sequence | Balance or gauge error |
Two deserve separating, because buyers misdiagnose them most often.
The part that measures correctly when new and loses force in service is usually suffering from cure, not structure. A coarse open structure collapses more readily, but the site ties a high compression set result to incomplete cure, and a shortened cure yields a part that measures near nominal when new and keeps changing afterwards.
Porosity is not a cellular structure. Intended cells are uniform and closed; porosity is uncontrolled voids, and moisture is the usual mechanism, because water reacts with isocyanate and releases carbon dioxide inside the part. A part with porosity can pass a hardness check and fail in fatigue, because the void is a stress raiser.
Specifying Microcellular Polyurethane on a Drawing
A drawing that states only hardness and geometry leaves the curve to chance. Nine fields close most of the gap, and all nine fit on one page.
Density and tolerance, with the measurement method, so both sides calculate the same number.
Part mass and tolerance, the field-level proxy for density that anyone can check.
Free height and tolerance, measured on the part rather than the mould.
Curve points at three deflections, with test speed and plate size.
Hardness and the measuring surface, since a rib reading is not comparable with a flat one.
Skin requirement, as continuous skin on the load face plus a section photograph.
Appearance zones, separating sealing and load surfaces from where a moulding mark is acceptable.
Batch record content, naming compound, cure and post-cure parameters and the curve result.
Change notification, so a compound or density change triggers a re-verified curve rather than an assumption.
The reason to put all nine on paper is arithmetic. The cost of catching a structure error rises with how late it is caught.
| Stage where the error is caught | What has to be done | Cost, illustrative |
|---|---|---|
| First article | 3.5 h at 65 USD/h: density on five parts, one section cut, curve at three points, batch records | 227.50 USD |
| Goods-in | 2.0 h inspection (130), full sort of 6,000 parts at 0.05 (300), return air freight (480), re-verification (227.50) | 1,137.50 USD |
| In service | 54 failures at 0.9 per cent, each 0.8 h at 55 USD/h plus 18.50 of claim handling | 3,375.00 USD |
The ratio is roughly 1 to 5 to 15: the same 3.5 hours of verification, spent earlier or later. Every figure is an illustrative model with stated assumptions rather than a quotation.
None of this needs a new test method. Bonpora inspects the stiffness curve, compression set, hardness and appearance on every batch sample under an IATF 16949 system, and states a working range of -40 °C to +90 °C with the material adjustable outside it. What the drawing adds is the density, the section reference and the mass tolerance that connect those existing checks to the structure producing the curve.
Where no reference exists, a custom bumper can be produced from a sample or a drawing. Agree the geometry and the required stiffness behaviour first, then select or adjust the compound to deliver it, rather than picking a density and hoping the curve follows. The reverse order is the usual reason a first article arrives with the right dimensions and the wrong feel.
Frequently Asked Questions
Can I specify microcellular polyurethane by density alone?
No. Density sets the level of the curve, but skin, cell size and profile decide its shape. Two parts at 0.52 g/cm³ can differ by a third at 25 per cent deflection if one has a thick skin and fine cells and the other a thin skin and a coarse core. State density, mass and curve points together, and attach a section photograph.
Why does a bumper read the right hardness and still sag after a season?
Hardness is a surface measurement taken when the part is new; sag is permanent deformation after long compression. That gap is normally compression set rather than cell structure, and it usually traces to an incomplete cure. Ask for the set result and the cure record for the batch rather than another hardness reading.
Is a lower-density part always softer near the top of the stroke?
No, and the inversion is worth knowing. A low-density part with a thick, well-formed skin can be firmer at small deflection than a denser part with a thin skin, because the first millimetres of travel load the skin rather than the core. Compare curves at three deflections and check where the knee falls.
Does cell structure change the temperature behaviour of microcellular polyurethane?
The gas in the cells and the polymer both respond to temperature, and stiffness rises as temperature falls. Bonpora states a working range of -40 °C to +90 °C for the on-road range and notes that the material can be adjusted outside it. If the part will be evaluated at both ends, ask for the curve at both.
How do I check density on a delivered carton without cutting a part?
Weigh five parts on a 0.01 g balance, measure the envelope with a calliper and divide mass by volume. On small parts the result runs slightly high because the skin is a larger share of the volume, so compare it with the first-article value measured the same way, not with a compound datasheet. A section cut is still needed to see the cells.
What is the difference between porosity and a cellular structure?
A cellular structure is intended, uniform and closed; porosity is uncontrolled voids, usually from moisture reacting with isocyanate or from incomplete degassing. Porosity can pass a hardness check and still fail in fatigue, because a void concentrates stress. Appearance inspection of the load and sealing surfaces is the quick screen, and a section cut is the confirmation.